sales06@switek.biz

+86 186 5927 5869

Shopping

Subscrib to Us
sales06@switek.biz
+86 186 5927 5869
Shopping
Subscrib to Us

Haitian, the wrold largest manufacturer of injection molding machine, on show their 5th generation of high precision servo injection molding machine MA1600 with top entry IML solutions for the production of shoehorn with degradable plastic at PlastImagen 2025.
Details of MA1600
| INJECTION UNIT | A | B | C | |
|---|---|---|---|---|
| Screw diameter | mm | 40 | 45 | 50 |
| Screw L/D ratio | L/D | 22.5 | 20 | 18 |
| Injection volume (theoretical) | cm3 | 253 | 320 | 395 |
| Injection weight (PS) | g | 230 | 291 | 359 |
| Injection Rate | g/s | 111 | 141 | 174 |
| Injection rate (ESG) | g/s | 150 | 190 | 235 |
| Injection Pressure | MPa | 225 | 178 | 144 |
| Plasticizing rate (GPPS) | g/s | 17.0 | 22.6 | 28.4 |
| Screw speed | rpm | 0~215 | ||
| CLAMPING UNIT | ||||
| Clamping force | kN | 1600 | ||
| Mold opeing stroke | mm | 430 | ||
| Dist. between tie bars (H x V) | mm | 470 x 470 | ||
| Mold height max. | mm | 520 | ||
| Mold height min. | mm | 180 | ||
| Ejector stroke | mm | 140 | ||
| Ejector tonnage | kN | 33 | ||
Tips for a Top Entry IML System with MA1600

SW6712S
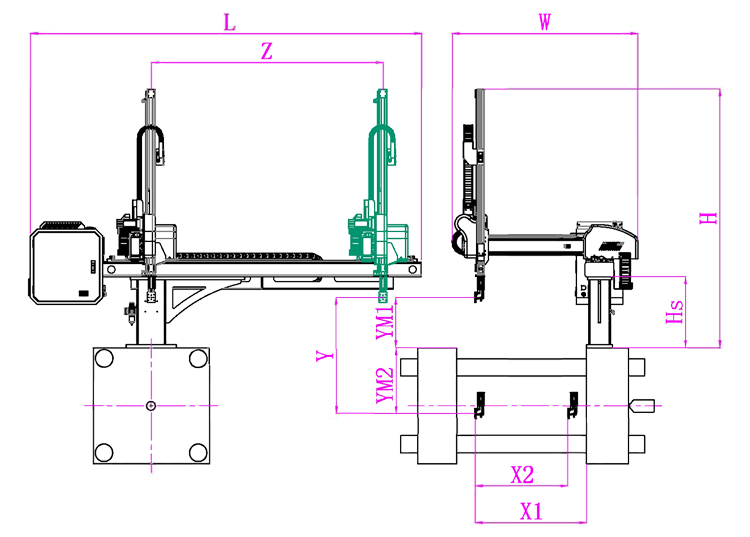
Unit: mm
| X1 | X2 | X3 | X4 | Y | YM1 | YM2 | Z | L | W | H | Payload | 900 | 840 | 0 | 0 | 1200 | 420 | 780 | 2000 | 3020 | 1610 | 2050 | 8kg |
|---|
EOAT Assembly Demonstration -- Two Cavities Parts Picking EOAT with Runner Gripping
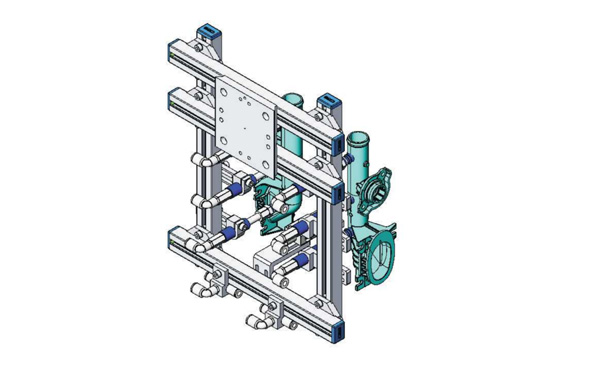
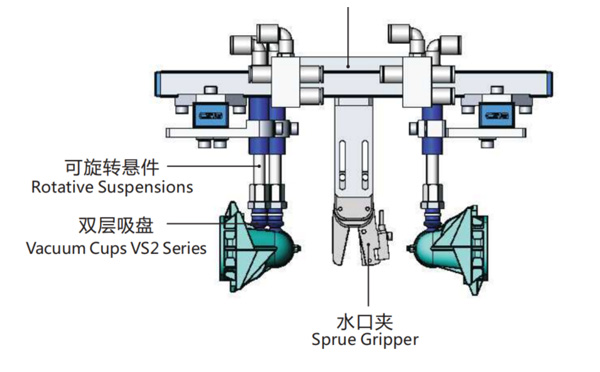
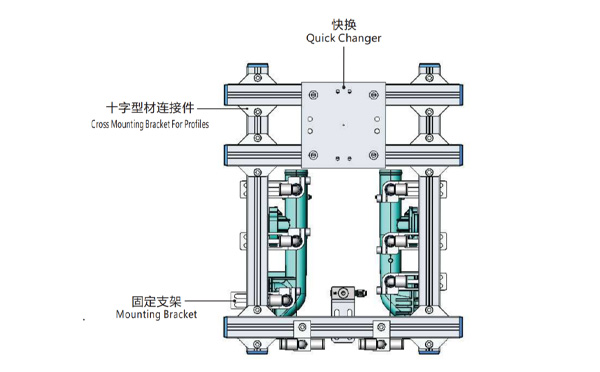
Product Descriptions
Bom List
| Product Name | PN # | Model | Quantity |
|---|---|---|---|
| Quick Changer | 7.Y00175 | QCS-G100 | 1 |
| Sprue Gripper | 8.Y00050 | GR12-12CP | 1 |
| Plugs for Profile | 4.Y00069 | PEP2518 | 10 |
| Cross Mounting Bracket for Profiles | 7.Y00194 | SMBA-2525T | 6 |
| Extruded Profile | 4.Y00455 | PEP2518-1000 | 2 |
| Vacuum Cups VS2 Series | 1.Y03085 | VS2-SA11 | 6 |
| Vacuum Cup Fitting | 7.Y00703 | VM-02-G18 | 6 |
| Rotative Suspensions | 8.Y00061 | VFR1421-G18 | 6 |
| Mounting Bracket | 7.Y00200 | SMBE1-1440T | 6 |
| Connector | 1.Y02510 | APF-M5 | 2 |
| Side Manifold Block | 7.Y00157 | SMB-06M5 | 2 |
| L-Type Threaded HOse Fitting | 1.Y02722 | APL6-01 | 8 |
| Straight Threaded Hose Fitting | 1.Y02725 | APC6-01 | 6 |
What's Would be the Most Economic Way to Produce An IML Bucket With Handle?
As one of the most popular food package in the market, an IML pail with handle is in demand of huge quantity but the assembly of the handle make it a labour entensive products. Is there any solutions that will make the production of an IML bucket with handle automatically? The answer would definitely yes.
One of the most economic way would be to have the pails and handle integrated into one single mold, it could be 2 + 2 or 4 + 4 design which the IML robot will pick the buckets and have the handles assembled automatically. With this solution, the IML buckets producer will only need one set of IML system to have the buckets and handle produced and assembled immediately.
> It sounds great right, but what would be the productivity of such a system? In Chinaplas 2024 SWITEK cooperated with YIZUMI onshowed a 2 + 2 IML solution of 1L pails at the cycle time of around 7.5s. Generally the performance of the injection molding machine, the mold and the IML robot are all very important to make it a perfect IML system with handle assembly.
Fore more questions about your IML projects, please feel free to contact Adams from SWITEK, your personal consultant of IML technology.