sales06@switek.biz

+86 186 5927 5869

Shopping

Subscrib to Us
sales06@switek.biz
+86 186 5927 5869
Shopping
Subscrib to Us

With the control system developed by the Austria automatic company SIGMATEK GmbH & Co KG, SWITEK high speed side entry IML robot is providing a more efficient and outstanding performance for your quality bulk production of the IML Yogurt Cups.
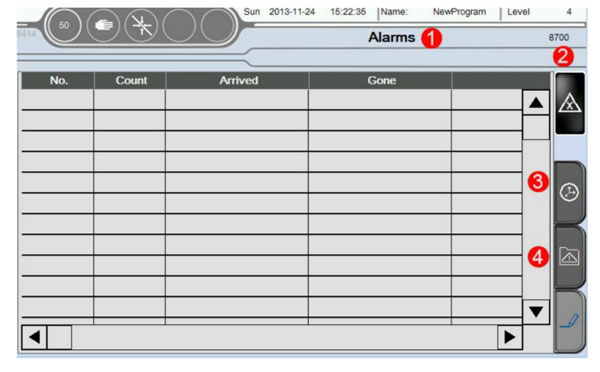
4.1 Alarms
Click Alarms button. As shown in the below picture of 1.6.1:
| No | Alarm | Illumination | Treatment |
|---|---|---|---|
| A004 to A015 | Axis Interior Min Limit | Indicates current actual limit is less than the set Min limit. | In the manual page, remove this axis to Min Limited Funcction/Servo Setup/Axis/**/Axis Assignment->Max Limited in program, actual limited must be more than this set value, suggestion for -1.00mm. |
| A021 to A032 | Axis interior Max limit | Indicates current actual limit more than the set Max limit | In the manual page, remove this axis to Max Limited Function/Servo Setup/Axis/**/Axis Assignment->Max Limited in program, actual limited must be less than this set value. This value is depended on the Mechanical Dimensions. |
| A041 to A052 | Axis position limit | Indicates axis' motion can not follow the speed of CNC instruction | -Function/Servo Setup/Axis/**/Axis Control Assignment-> Max limited deviation, the first value is set 10mm more than the second. The second show the current actual deviation, suggested to adjust driver's rigidity to decrease deviation. -Function/Servo Setup/Axis Assignment/**/Axis Control Assignment -> advance the value of KV, VU, suggested to advance 50 each time -adjust accelerated speed, Function/Servo Setup/Axis configuration |
| A061 to A072 | Axis Alarms | Indicates breakdown happens inthe current axis** | -Axis control module (CST 022/CNC 305/CNC 115 and so on) has not been tested -+24V/+5V power supply of Axis control module is abnormal -Check the corresponding limiting point configuration of I/O |
| A081 to A092 | Axis position Min limit | Indiccates that there is signal inputting in the Minimum limit sensor of current axis | -mechanical hand is located in the position beyond limit Check machine -misdescription happens in the transducer. Check transducer -Check the corresponding limiting point configuration of I/O |
| A101 to A112 | Axis position Max limit | Indicates that there is signal inputting in the Maximum limit sensor of currrent axis. | -mechanical hand is located in the position beyond limit. Check machine -misdescription happens in the transducer. Check ransducer -Check the corresponding point configuration of I/O |
| A121 | Emergency stop button Pressed down | Emergency stop of machine active on the Control panel. | -Rotate the Emergency stop of machine chockwise to loosen it/System Setup. function is , so this Emergency will not appear until Reboot; if check . Emergency disiappear automatically. -If Button Stop of hand controller virtual key is pressed down, reset this virtual key. |
| A122 | Pressure abnormal | pressure abnormal | Check pressure. Check wether or not pressure test has been turned on. |
| A123 | Emergency stop of machine active | Checked Emergency stop of machine put down |
|
| A124 | Safety equipment is abnormal | Machine safety door open |
|
| A125 | Quantity accomplished | Set quantity has been finished | Function/produce setup page->Quantity Setup |
| A126 | Reject part reaches setting limit | Amount of reject part has reached the number of set alarms | function/produce setup page - > Reject Alarm Interval |
| A127 | Cycle time overtime | Cyclical time exceeds the safety time scope. | function/produce setup page -> motion monitor time; 0 do not means monitor. |
| A128 | Fixture abnormal | Fixture motion beyond the set time of monitor |
|
| A129 | Module Open/Close signal abnormal | Conflict between Module Open and Module Close |
|
| A130 | Vacuum abnormal | Monitor of Vacuum exceed the set monitor time. |
|
| A131 | Division by zero error | Set parameter has been divided by 0. | Check whether set parameter has been divided by 0. Set parameter is too small. |
| A133 | Module Open Interval Time | Interval is too short between two Module Open |
|
| A141 to A149 | Baseboard slot modulel error | The order error in the second module Baseboard …… the order error in the ninth module Baseboard |
|
| A150 | CIV512 module error | Order of CIV 512 module tests wrong. |
|
| A151 A152 | Driver module | Order of Driver SDD/MDD tests wrong. Driver 1: PLC varan bus connects with the driver firstly; Driver 2: bus connects with this driver secondly |
|
| A161 | Module Open pattern Interval abnormal | Interval between the two Module Open Receive signal is too short |
|
| A162 | The label paper shortage | System receives the signal of label paper shortage |
|
| A163 | VBC error | The order of VBC module is tested wrong |
|
| A171 to A203 | Motion overtime | Automatic running, the motion time of corresponding axis exceeds safety time. |
|

SW6310S-20
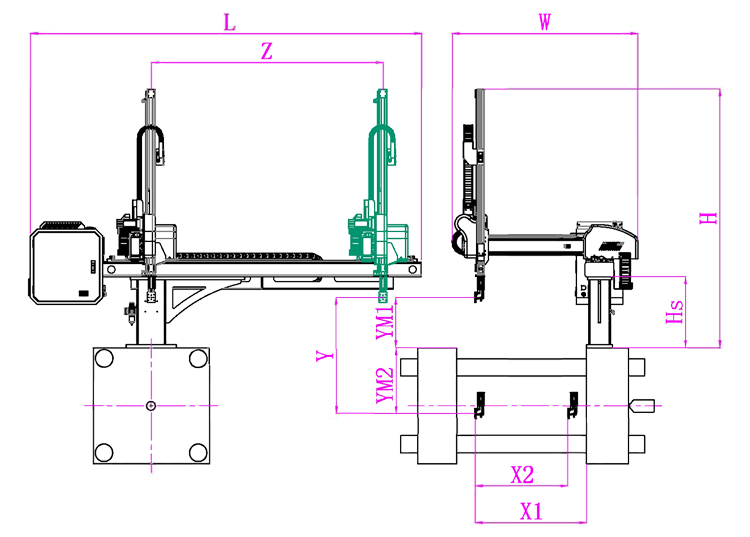
Unit: mm
| X1 | X2 | X3 | X4 | Y | YM1 | YM2 | Z | L | W | H | Payload | 980 | 820 | 0 | 0 | 1000 | 235 | 765 | 1580 | 2640 | 1500 | 1930 | 3kg |
|---|
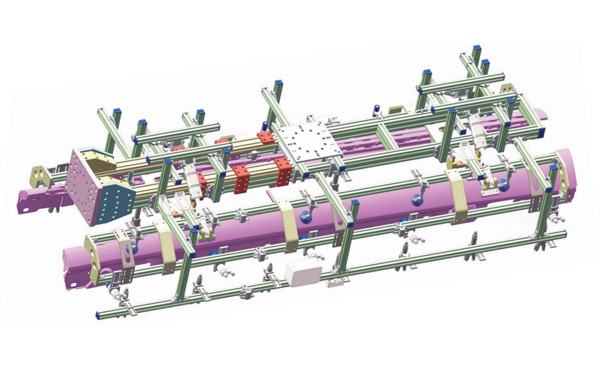
EOAT Assembly Demonstration -- One Cavity Car Threshold Strip Picking EOAT
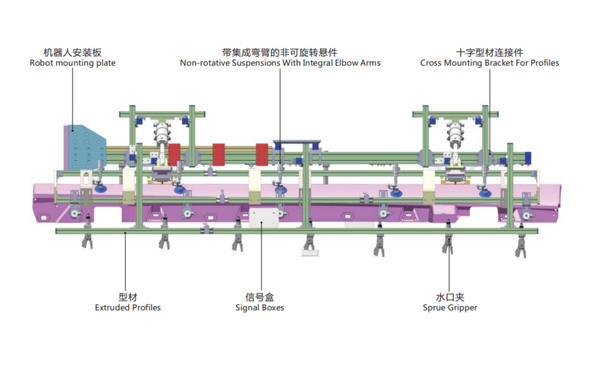
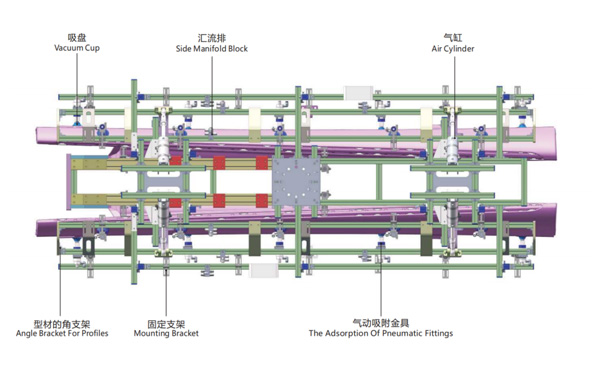
Product Descriptions
Is there any Low Budget Solutions for PVC Pipe Fittings Runner Cutting?
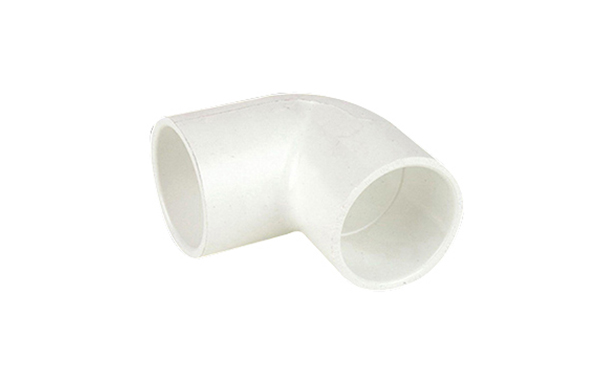
PVC pipe fittings are one of the most commonly used connector in the drainage project and a cold runner designed mold is the most economic solutions for the production of the PVC pipe fittings, but the removal of the runner in result is a labour intensive work. Is there any economic way to remove the runners from the PVC pipe fittings automatically?
For the producer of PVC pipe fittings the most economic soluton to remove the runner is with an Air Nipper fixed to the picking robot immediately after the PVC pipe fittings picked out from the mould. The robot will drop the seperated pipe fittings and runner to different containers. Below configuration of SWITEK runner cutting solution for 16 cavities PVC pipe fittings for your reference:
The Air Nipper runner cutting system is an easy to start solution for the producers of PVC pipe fittings, which the Air Nipper would be controlled by the picking robot and is the best solution for the small size PVC pipe fittings (with a diameter around φ25mm). Anyway it also must be custom made according to the mold design.
For more solutions about the pipe fittings runner cuttings and other automation solutions please contact Adams from SWITEK, for a profound proposal of turn-key solutions of pipe fittings production.